
7 Tips for Choosing the Right Aluminum Can Lid
Choosing the right Aluminum Can Lid is a small decision with visible consequences. A weak seal can leak during transport. A poor opening design can frustrate customers at the first sip. The lid must work quietly, even when the can faces heat, vibration, moisture, and pressure.
“Every lid is a promise that the contents will arrive as intended,” says packaging consultant James R. Sapp. His reminder captures the practical purpose of an Aluminum Can Lid. It is not merely a metal component. It supports product protection, opening comfort, brand presentation, and production efficiency. The correct choice depends on more than diameter. Material thickness, coating quality, tab design, scoring accuracy, seal performance, and compatibility with filling equipment all deserve attention.
Details matter.
This guide presents seven practical tips for comparing Aluminum Can Lid options. It considers the product inside, the can format, manufacturing conditions, and the customer’s hand. A carbonated drink may require different performance than a still beverage. A premium product may benefit from a smoother tab and cleaner finish. Cost also matters, but the cheapest lid may create waste, complaints, or line stoppages later.
No checklist is perfect. I have seen specifications look convincing on paper, then fail during real handling. Testing remains essential. Examine samples under pressure, inspect the seal after filling, and review opening performance with actual users. Reliable decisions come from evidence, not attractive claims.
Define the Can’s Purpose and Required Lid Features
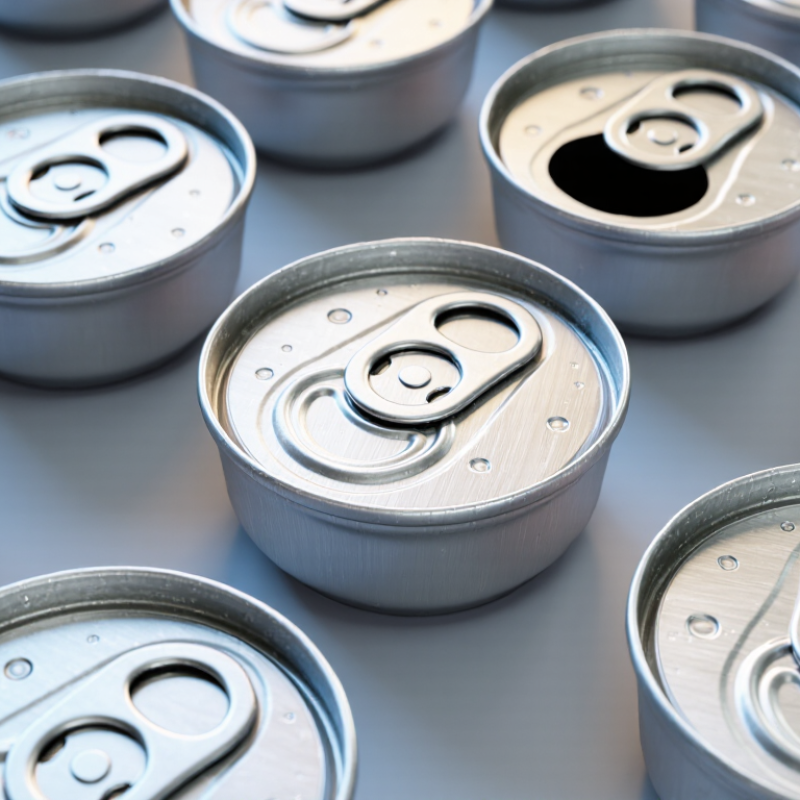
Before choosing an aluminum can lid, define what the can will hold and how people will use it. A lid for sparkling drinks needs reliable pressure resistance and a clean opening. A lid for dry powders may need stronger protection against humidity. The contents matter most.
Think about the storage environment, too. Will the can sit in a warm warehouse, a cold truck, or a damp bathroom? Temperature changes can stress the seal. Frequent handling may require a lid with a firm pull tab and a smooth rim. For products used outdoors, consider dust protection and easy opening with wet hands. Small details affect customer experience.
I usually check the lid’s diameter, sealing compound, panel strength, and opening force. These features should match the can body, not merely look compatible. Food or beverage applications also require suitable contact materials and documented quality testing. Ask for pressure, leakage, and corrosion data when relevant. Numbers are more useful than confident promises.
I once treated an easy-opening design as automatically better, but some users found the tab difficult to grip. That mistake changed my evaluation process. Now I test samples with different hand sizes and realistic storage conditions. A lid can perform well in a laboratory and still feel awkward in daily use. Testing should include both measurable performance and practical handling.
