
China Top Chinese Laid Scrims Mesh Manufacturer Supplier
China has become an important sourcing base for industrial reinforcement materials. Chinese Laid Scrims Mesh supports roofing membranes, insulation, flooring, packaging, and composite products. Its open structure adds dimensional stability without creating unnecessary weight.
A capable Chinese manufacturer begins with the application, not only the order quantity. Production teams review yarn type, mesh size, roll width, tensile requirements, coating needs, and installation conditions. Fiberglass, polyester, and other yarn options can serve different performance targets. Samples should be checked before mass production. Width, mesh spacing, roll tension, bonding strength, and appearance all matter.
Reliable suppliers use controlled weaving or laying processes and practical inspection records. They should explain tolerances clearly. They should also provide traceable batch information and consistent export documentation. Factory communication matters. A small misunderstanding about coating or core diameter can disrupt an entire production line. That detail is easy to underestimate.
The best supplier is not always the lowest-priced one. Material consistency, response speed, packaging quality, and technical support often affect the final cost. No product suits every project. This point deserves honesty. Buyers should compare samples under real processing conditions, rather than trusting a brochure alone. An experienced Chinese supplier can help adjust specifications, but final approval should remain evidence-based. This guide examines China’s leading Chinese Laid Scrims Mesh manufacturers and suppliers, with attention to quality control, customization, production capability, and dependable long-term cooperation.
What Is Chinese Laid Scrims Mesh?
What Is Chinese Laid Scrims Mesh?
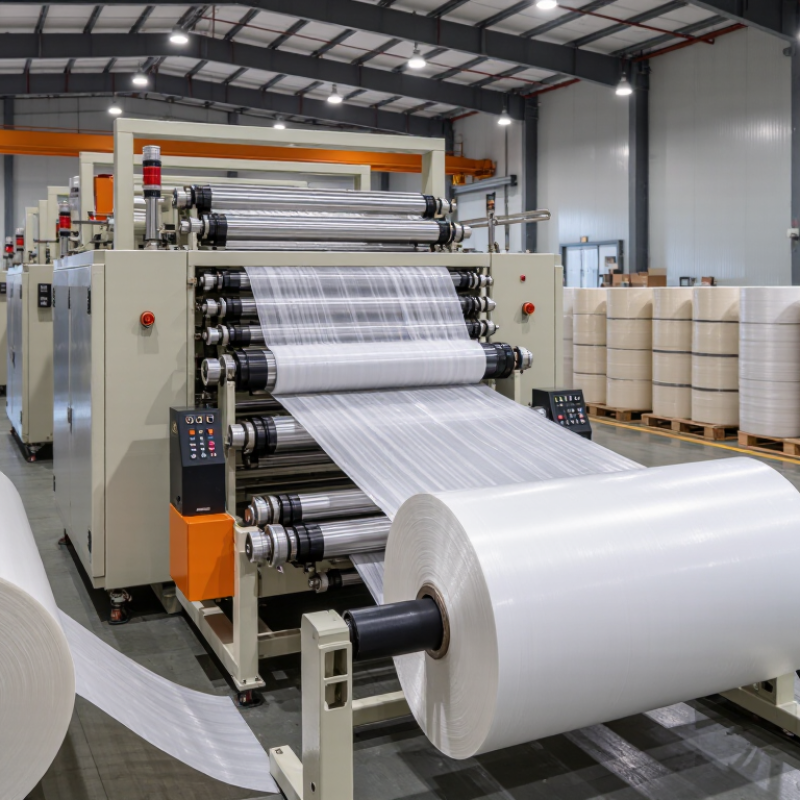
Chinese laid scrims mesh is a reinforcement fabric made by placing yarns in a grid pattern. The yarns are not woven over and under each other. Instead, longitudinal and crosswise strands are arranged flat, then bonded with adhesive. This structure creates low weight, stable dimensions, and useful tensile strength. It is commonly placed inside roofing membranes, insulation facings, wall coverings, flooring materials, and composite sheets. The open mesh allows coatings to pass through more easily. That improves reinforcement without adding unnecessary bulk.
Manufacturing quality depends on yarn selection, spacing, bonding strength, and roll consistency. Common yarns include fiberglass, polyester, and other engineered materials. Fiberglass offers strong dimensional stability, while polyester can provide flexibility during handling. Chinese suppliers often produce custom widths, mesh openings, roll lengths, and coating levels. However, specifications on paper are not enough. Uneven adhesive coverage can cause weak points. A careful buyer should request samples and test them under actual working conditions.
Tips: Check mesh count, yarn direction, tensile strength, and bonding uniformity. Inspect the roll for wrinkles, broken strands, and loose edges. Small details matter. It is also wise to confirm storage conditions, because moisture and heat may affect performance. The cheapest option may not be the most reliable. A better decision compares test results, production control, and application requirements. Some assumptions fail in real installation, so practical testing remains essential.